Serving rich, milk-based winter beverages presents unique challenges for cafes and restaurants. Unlike standard black coffee, cocoa drinks are often thicker, served at high temperatures, and heavily topped with cream or marshmallows. To deliver this decadent experience flawlessly, sourcing a specialized hot chocolate takeaway cup is essential. The right packaging not only preserves the beverage's temperature but also enhances the customer's overall comfort and brand perception during cold weather.
As a proud manufacturing arm of the global APP Group, we have engineered hot beverage packaging that addresses these specific operational needs. We utilize a fully integrated supply chain, starting directly from our own sustainably managed forests. This allows us to extract premium PEFC-certified virgin pulp. Because we avoid weak recycled fibers, our cups feature exceptional structural integrity, preventing the base and sidewalls from softening when exposed to high-heat dairy liquids for extended periods.
Safety is equally paramount. In the past, moisture barriers relied heavily on perfluorinated chemicals. We prioritize consumer well-being by manufacturing every hot chocolate takeaway cup with a verified PFAS-free guarantee. Validated by EU ISEGA and US FDA standards, our products utilize advanced, eco-friendly water-based coatings. This means your customers can enjoy their warm beverages without the risk of harmful substances leaching into their drinks.
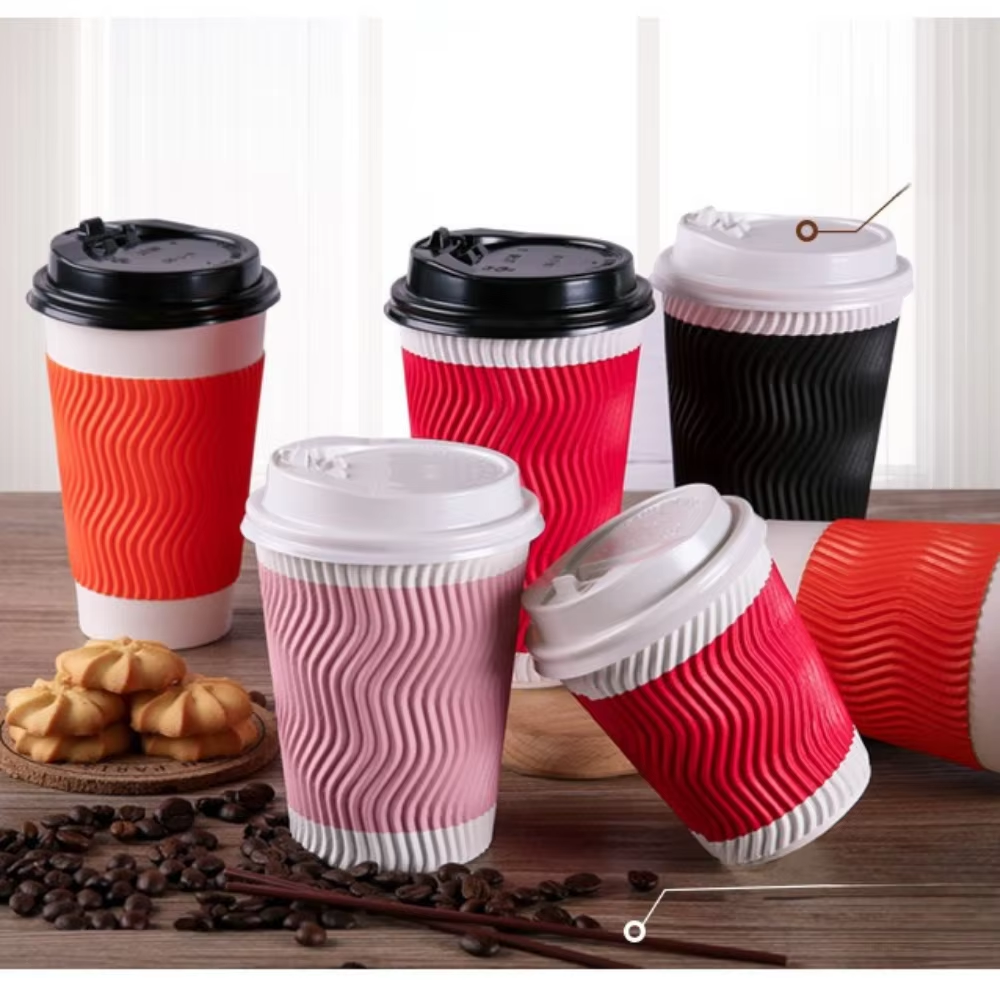
Furthermore, the physical design dictates its success. We specialize in double-wall and corrugated ripple-wall constructions that trap air, providing outstanding thermal insulation. This eliminates the need to purchase separate paper sleeves, reducing inventory costs. With over 200 automated converting lines, we provide vibrant, custom-printed cups featuring precision-rolled rims for tight dome lid sealing. By partnering with our SMETA-audited facilities, your brand secures a reliable, high-quality solution for the busy winter season.